
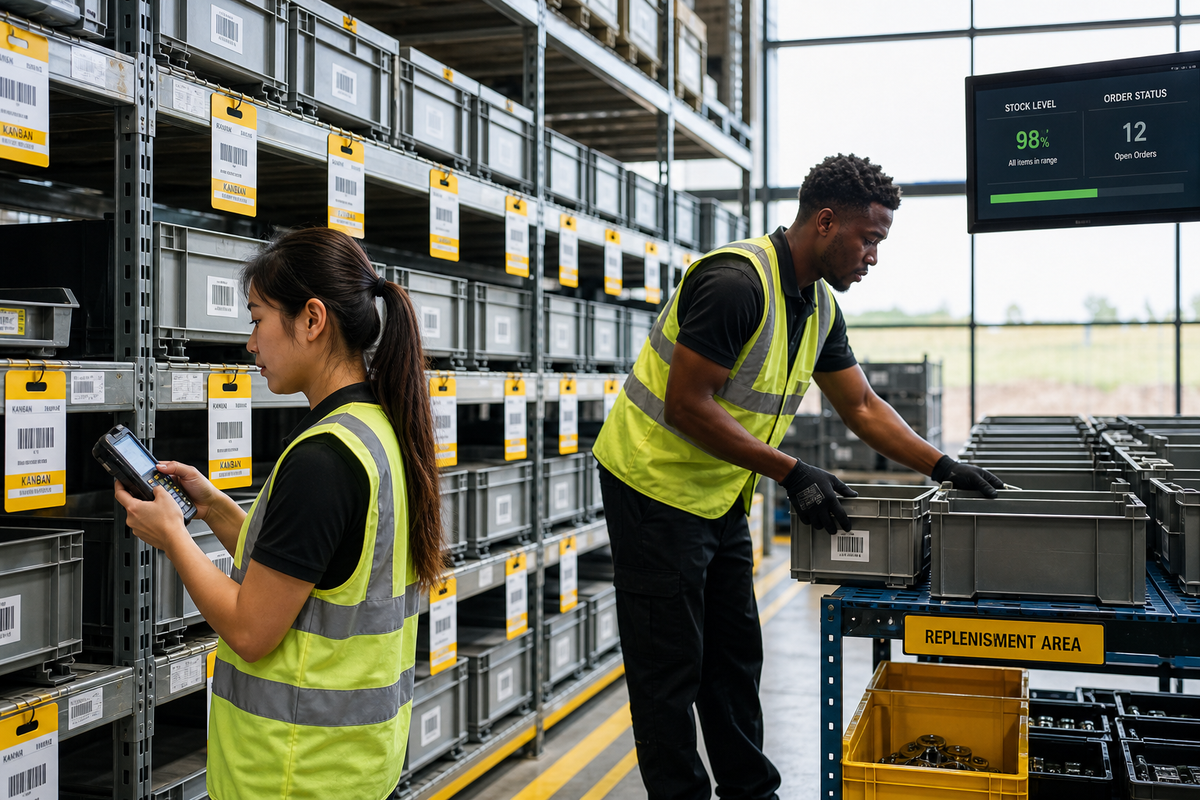
Kanban in the warehouse links consumption signals with predictable replenishment and reduces search times, missing parts, and excess inventory.
What Kanban Can Achieve in the Warehouse and Where It Makes Sense
When materials are missing from the warehouse or the production line, it often triggers a chain of inquiries, search efforts, and rush shipments. Kanban can stabilize this process through a simple pull principle: consumption triggers replenishment. Instead of reacting to forecasts or requests, the upstream process supplies exactly the quantity that the downstream process has actually withdrawn.
This is particularly helpful for warehouses and manufacturing when items are consumed regularly, containers are standardized, and there is a recurring flow between supply and consumption. Typical applications include small parts, packaging materials, assembly components, consumables, and internal replenishment warehouses. Kanban does not replace all inventory planning. It creates a clear control loop for those materials whose demand arises relatively regularly and is visible.
The basic principle is easy to explain: A container is emptied at the point of use. The associated card or a digital signal signals the need. The upstream area refills the container with the specified quantity and returns it to the designated location. This links material movement to information. Kanban is described as a consumption-oriented supply system in which quantity and timing are aligned with actual demand.
The advantage lies not only in lower inventory levels. A well-functioning Kanban control loop makes responsibilities transparent, reduces the need for follow-up inquiries, and supports a consistent workflow. At the same time, deviations are detected more quickly: If a container remains empty for too long, consumption does not match the standard, or a signal is not processed, this becomes immediately apparent in the process.
To ensure that Kanban in the warehouse does not simply become a place to store cards, it requires a suitable scope of application, clear labeling, and a mandatory response to every signal. The method is simple—its effectiveness stems from consistent standards.
Setting Up Kanban Control Loops: Containers, Signals, and Replenishment
A Kanban system becomes understandable on the shop floor through three elements: a clearly identifiable container, a clear signal, and a defined response. The container can be a bin, a pallet, or a shelf. The signal can be triggered by a card, a barcode, a QR code, or a digital notification. What matters is not the technology, but clarity: as soon as a unit is removed or becomes empty, everyone involved must know what is to be replenished, in what quantity, and by when.
For implementation, a limited control loop is recommended. A consumption point is linked to a replenishment area; both sides are assigned specific storage locations. The Kanban card must include at least the item number, description, quantity, withdrawal location, return location, and replenishment source. In digital versions, this information is stored in the system, but physical labeling remains important. Employees must be able to quickly identify the correct container.
The replenishment rule should be as simple as possible. Empty containers and a signal are returned to the upstream process; this process then provides exactly the defined quantity. LeanBase describes Kanban as an information impulse between processes, thereby emphasizing the feedback loop of consumption and replenishment. For warehousing and production, this means: It is not an assumption about demand that triggers movement, but actual consumption.
Even exceptions require a standard. What happens in cases of urgent demand, damaged containers, or missing materials? An escalation signal should be clearly distinguishable from the normal Kanban. Otherwise, special cases become the new normal, and the system loses its control function.
Key Metrics, Standards, and Continuous Improvement
A few well-chosen key performance indicators reveal whether Kanban is effective in the warehouse. These include the missing-part rate, replenishment time, search time, inventory turnover, number of urgent shipments, and inventory accuracy at consumption points. Baseline values are recorded before the pilot launch; after a few weeks, the system is checked to see if the control loop has stabilized. The key performance indicators should not become additional red tape, but rather highlight deviations.
A common mistake is to determine the number of Kanban containers based solely on average consumption. Replenishment time, consumption fluctuations, transport frequency, and an appropriate safety factor must also be taken into account. Too few bins lead to missing parts and rush orders; too many tie up space and capital. Therefore, the quantities must be regularly adjusted to actual consumption levels.
Kanban also works only with a stable foundation. Items must be clearly labeled, containers standardized, and storage locations visibly marked. If material quality, lead time, or process capacity fluctuate significantly, the root cause must first be addressed. The principle does not replace process stability; rather, it makes instability more quickly recognizable.
After the pilot, the system can be expanded to other areas. A common standard for cards, colors, storage location markings, and escalations should apply. Just-in-Time also aims for demand-driven provision in terms of quantity and timing. Kanban is therefore not an isolated card project, but a practical building block for lean, transparent material flows.
